GI Tagged Makhana
12,000+ Sq. Ft. Processing Plant • Katihar, Bihar

Industrial Roasting & Processing Pipeline

Operating in the heart of Bihar’s makhana cultivation belt since 2005. Take a transparent look inside our multi-stage sorting, zero-oil hot-air convection roasting, automated micro-mist seasoning, and continuous nitrogen sealing lines.
12,000+Sq. Ft. Built Campus
2005Harvest Legacy
USFDARegistered Plant
100%Oil-Free Convection
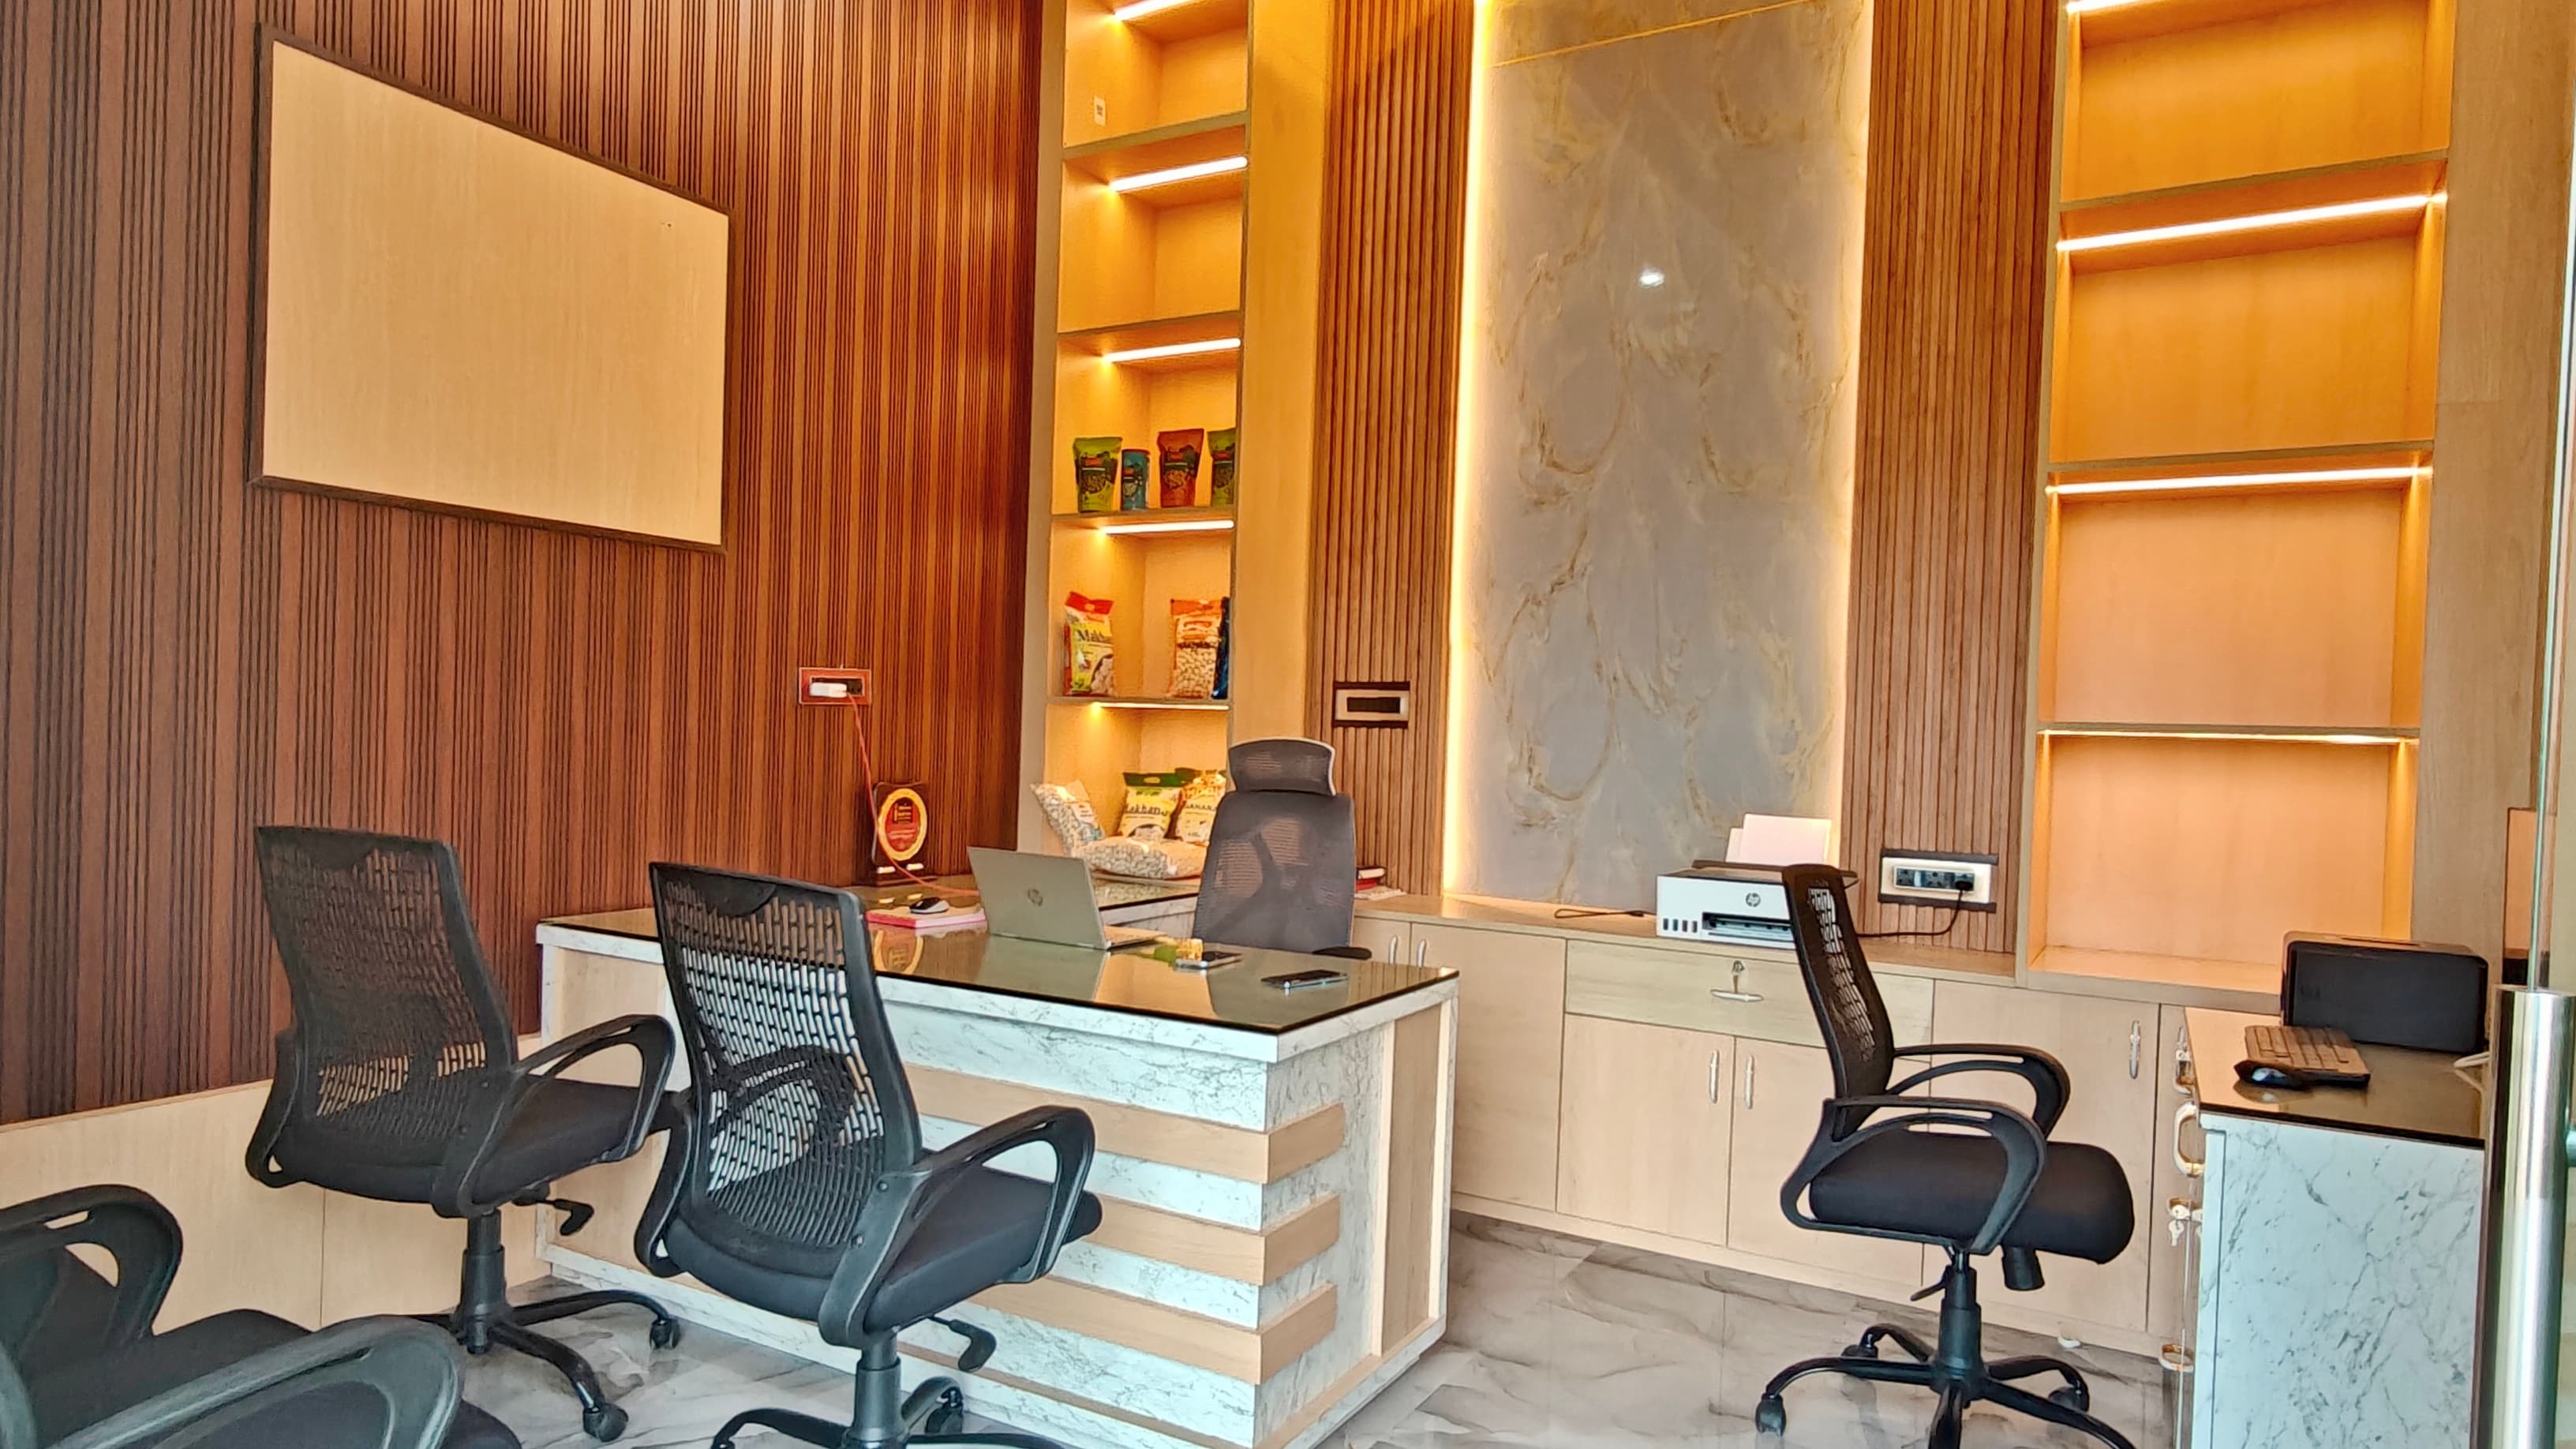
State-of-the-Art Processing Plant in Katihar, Bihar
Administrative & Plant Campus • Katihar Inspect Photo
Direct Roaster Advantage

State-of-the-Art Processing Plant in Katihar, Bihar

Located directly within the fertile makhana harvest heartland of Katihar, our 12,000+ sq. ft. industrial facility bridges rural farm ponds with international export shelves. By processing within hours of raw harvest, we eliminate middlemen, prevent transit moisture spoilage, and guarantee 100% farm-to-pack integrity.

12,000+Sq. Ft. Built-up Floor
100%Oil-Free Roasting
USFDARegistered Plant
< 3.5%Moisture Guarantee
Chronological Engineering Flow

The 9-Stage Roasting & Packaging Pipeline

Explore our end-to-end industrial manufacturing flow in Katihar, Bihar. Each station is operated under standardized Hazard Analysis Critical Control Points (HACCP) and ISO 22000 protocols.
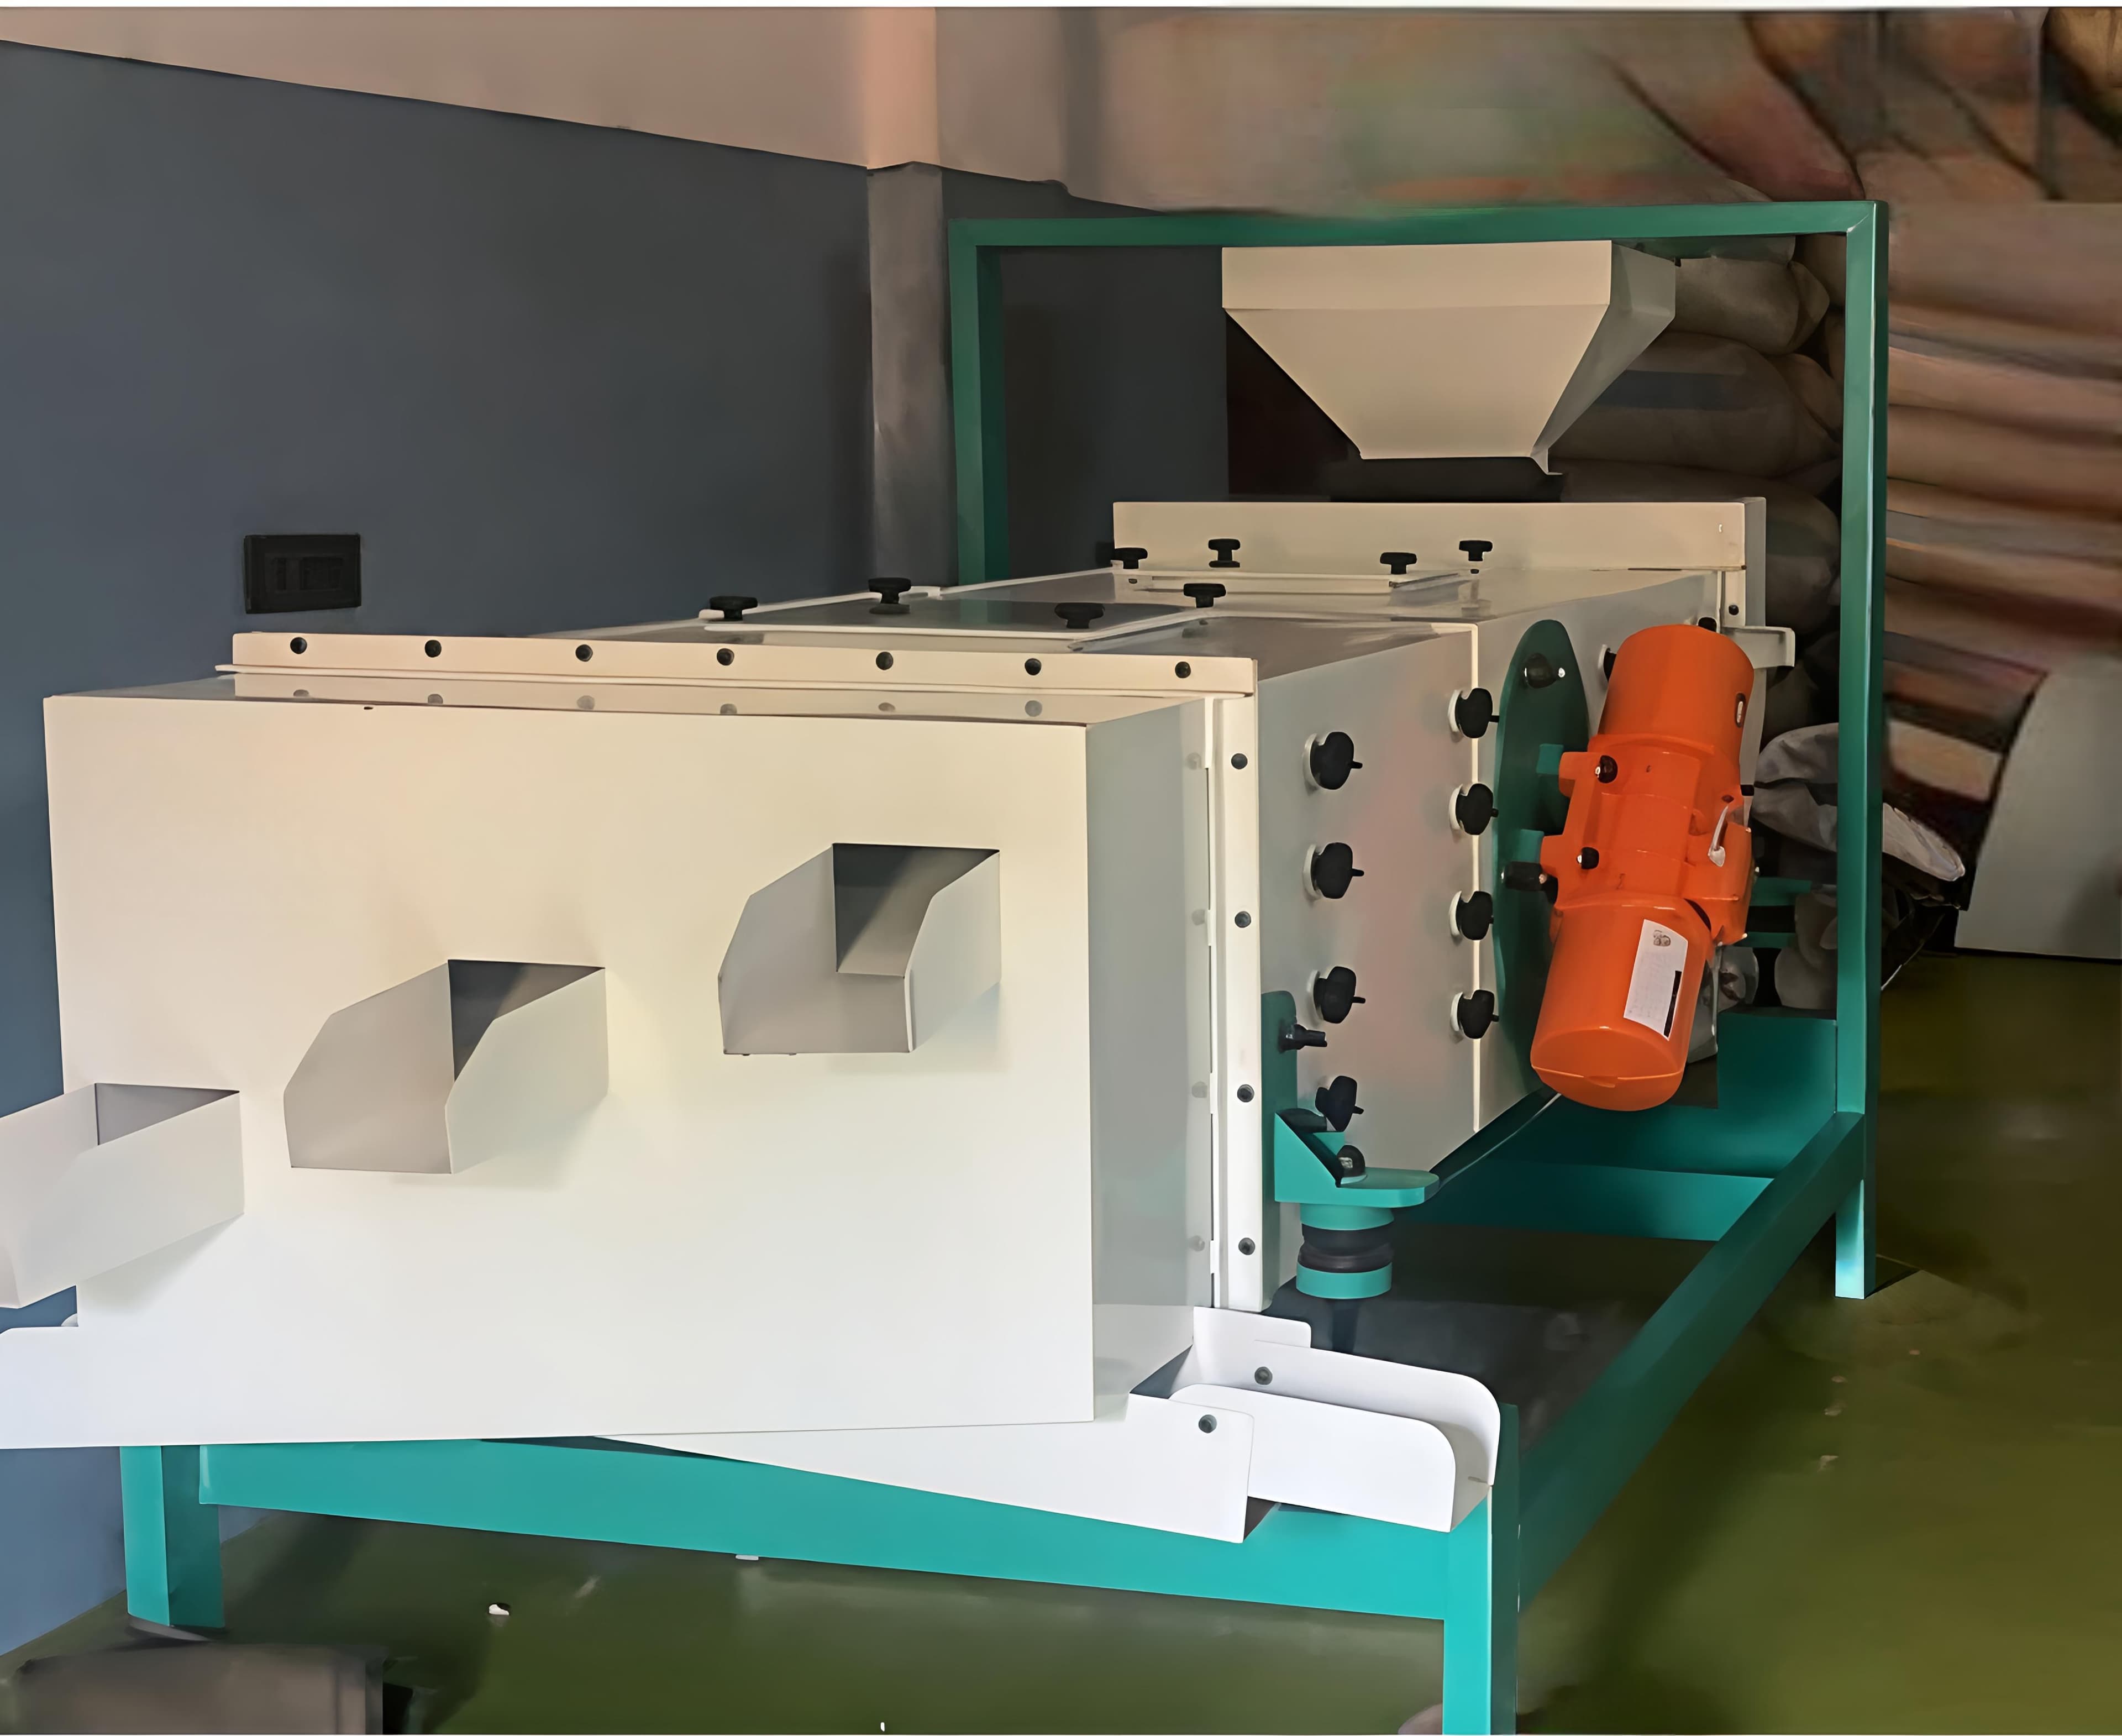
Mechanical Size Grading & Pre-Cleaning
Stage 01 • Raw Material SortingQuality Control Gate 1
EquipmentMulti-Deck Mechanical Vibratory Sizing Separator
01SOP-RAW-01 / Grade AAA Spec
99.8% Purity Sort Ratio

Mechanical Size Grading & Pre-Cleaning

Operating on calibrated vibratory oscillation sieves, raw popped foxnuts are separated by precise kernel diameter. Mechanical airflow dedusters remove microscopic husk particles and immature popped seeds, ensuring only pristine, uniform spheres move forward into the thermal roasting lines.
Grading Range4+ Soot (13-16mm) to 6+ Soot (20mm+)
Dedusting Efficiency99.8% Husk & Shell Removal
Processing Capacity500 kg / hour Continuous Feed
Material ContactFood-Grade SS 304 Contact Surfaces
Standardized Factory SOP
Precision Hot-Air Convection Roasting
Stage 02 • Thermal RoastingCritical Control Point (CCP-1)
EquipmentContinuous Multi-Zone Hot-Air Roasting Lines
02SOP-RST-02 / Thermal Curve Reg.
Zero Oil Roasting (100% Convection)

Precision Hot-Air Convection Roasting

Unlike commercial deep-fried snacks, our industrial convection roasting tunnels circulate precision-controlled dry laminar hot air across rotating conveyor beds. This non-contact roasting uniformizes internal moisture extraction, achieving an ultra-crisp fracture without caramelizing or scorching the foxnut albumen.
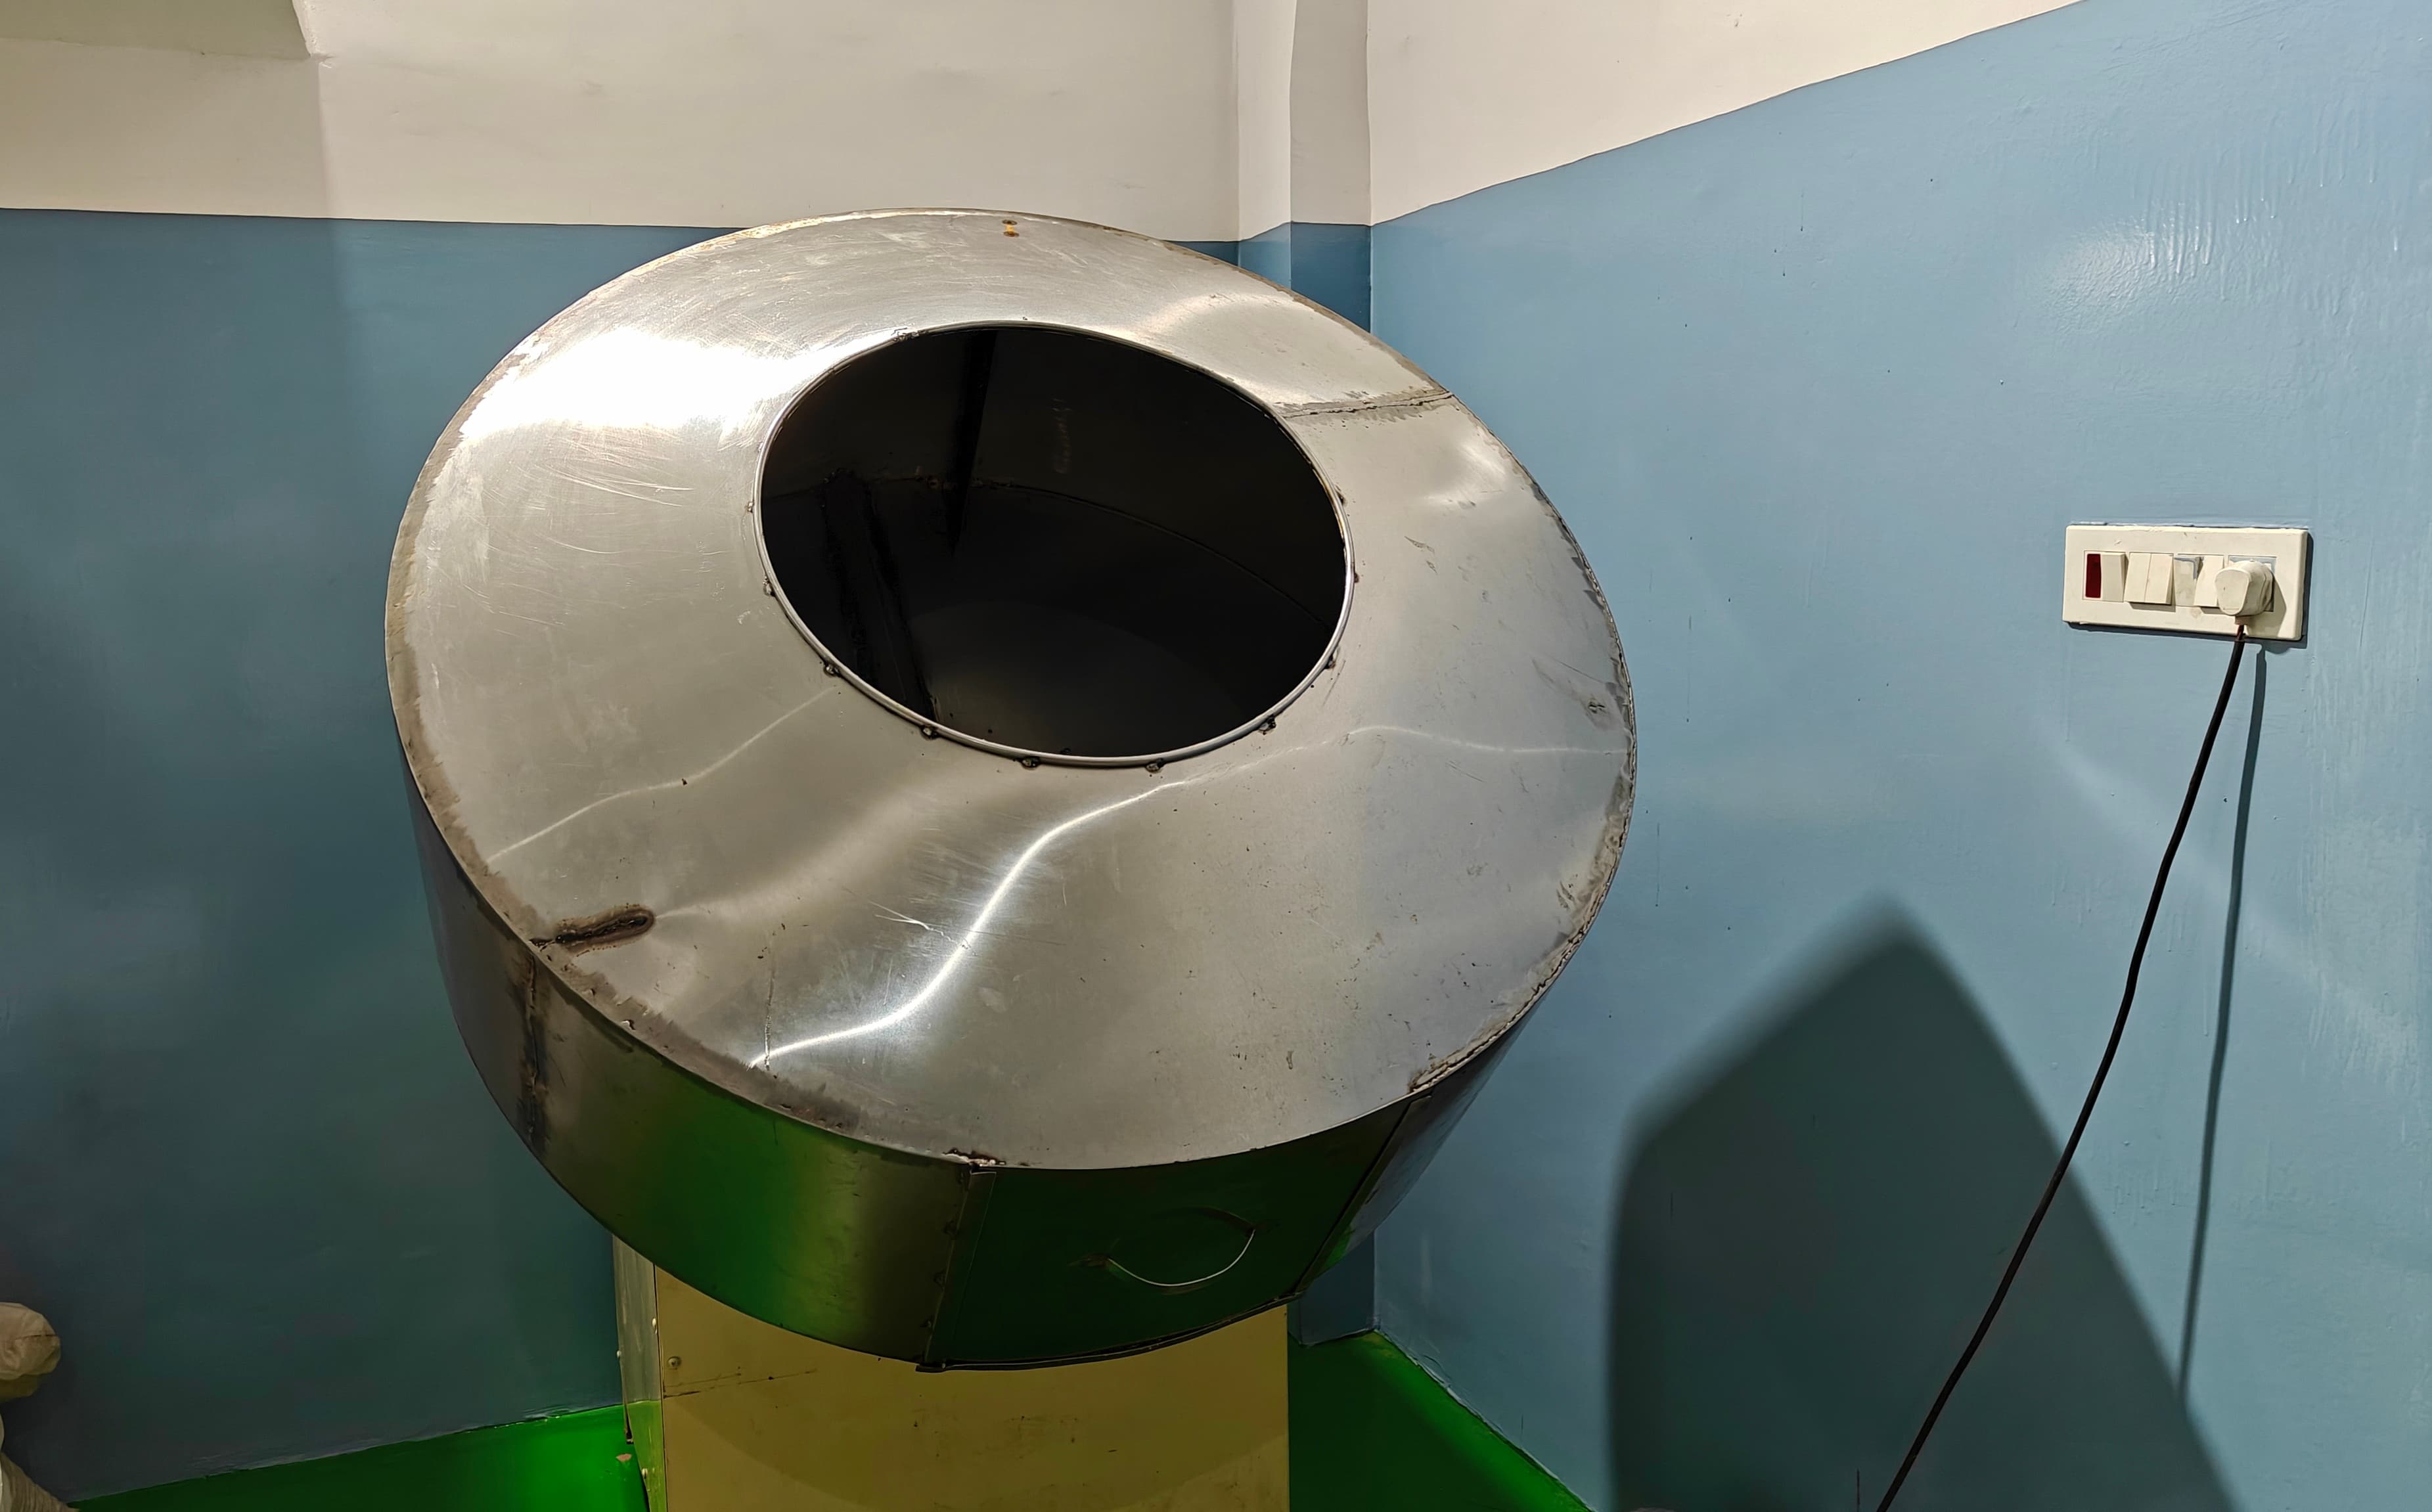
Roasting MethodDry Forced-Air Convection (0% Oil)
Temperature ControlMulti-Zone Digital PID Loop (±1.5°C)
Retention TimeVariable Speed Bed (8 to 14 Minutes)
Nutrient Retention9.7g Natural Plant Protein Preserved
Standardized Factory SOP
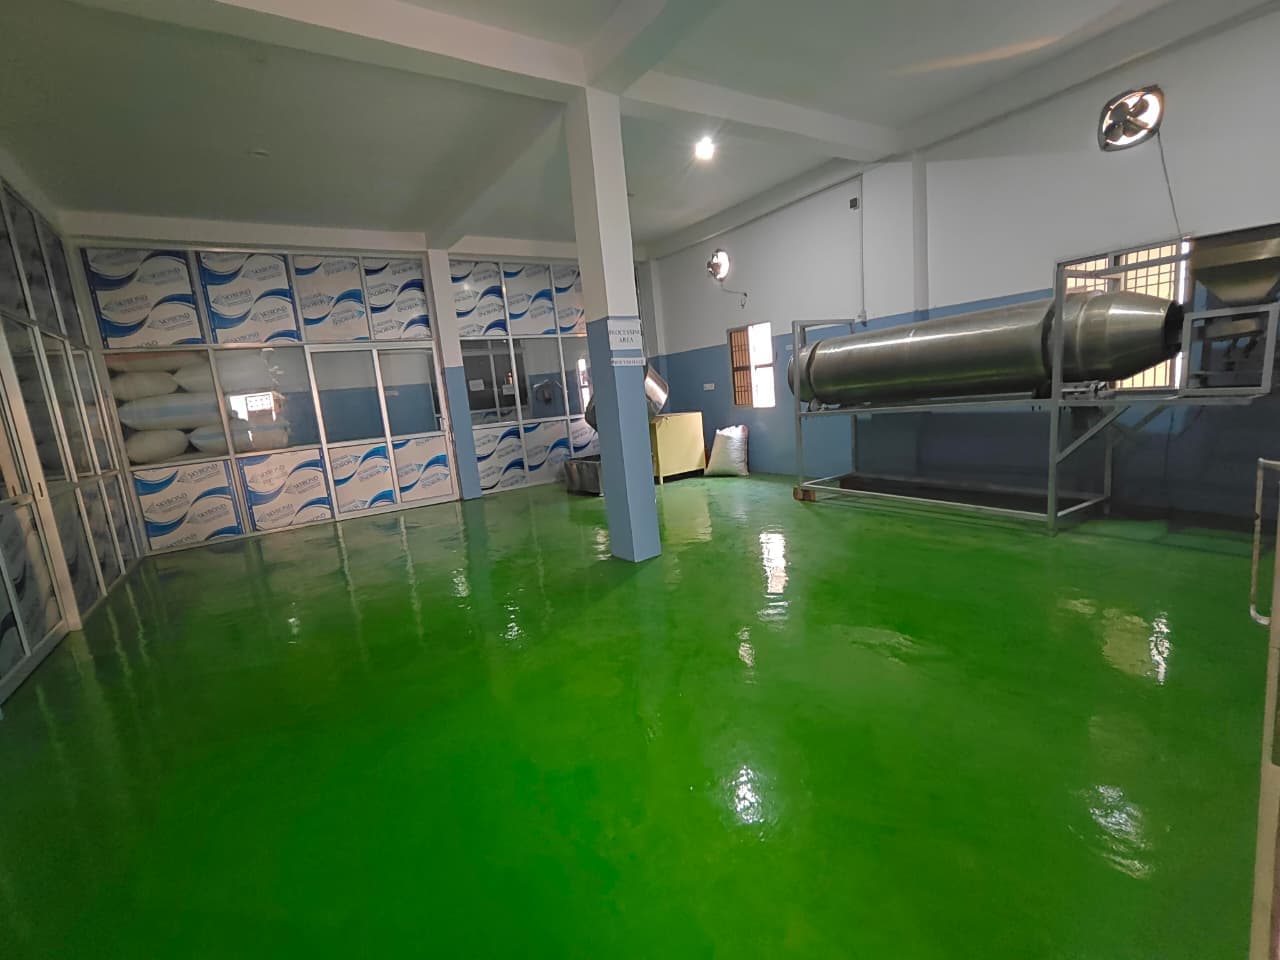
Automated Micro-Mist Tumbling & Seasoning
Stage 03 • Flavor InfusionSensory & Coating Gate
EquipmentRotary Stainless Steel Seasoning Tumbler & Atomizer
03SOP-FLV-03 / Batch Formulation Spec
Uniform 360° Spice Adhesion

Automated Micro-Mist Tumbling & Seasoning

Freshly roasted foxnuts enter a continuous rotary stainless steel coating drum. High-pressure atomizing nozzles disperse a micro-mist of cold-pressed oil, immediately followed by electro-vibratory spice feeders dispensing proprietary seasoning blends (Himalayan Pink Salt, Peri Peri, Cream & Onion, Mint, Tangy Tomato, etc.) for flawless 360-degree adhesion without breakage.
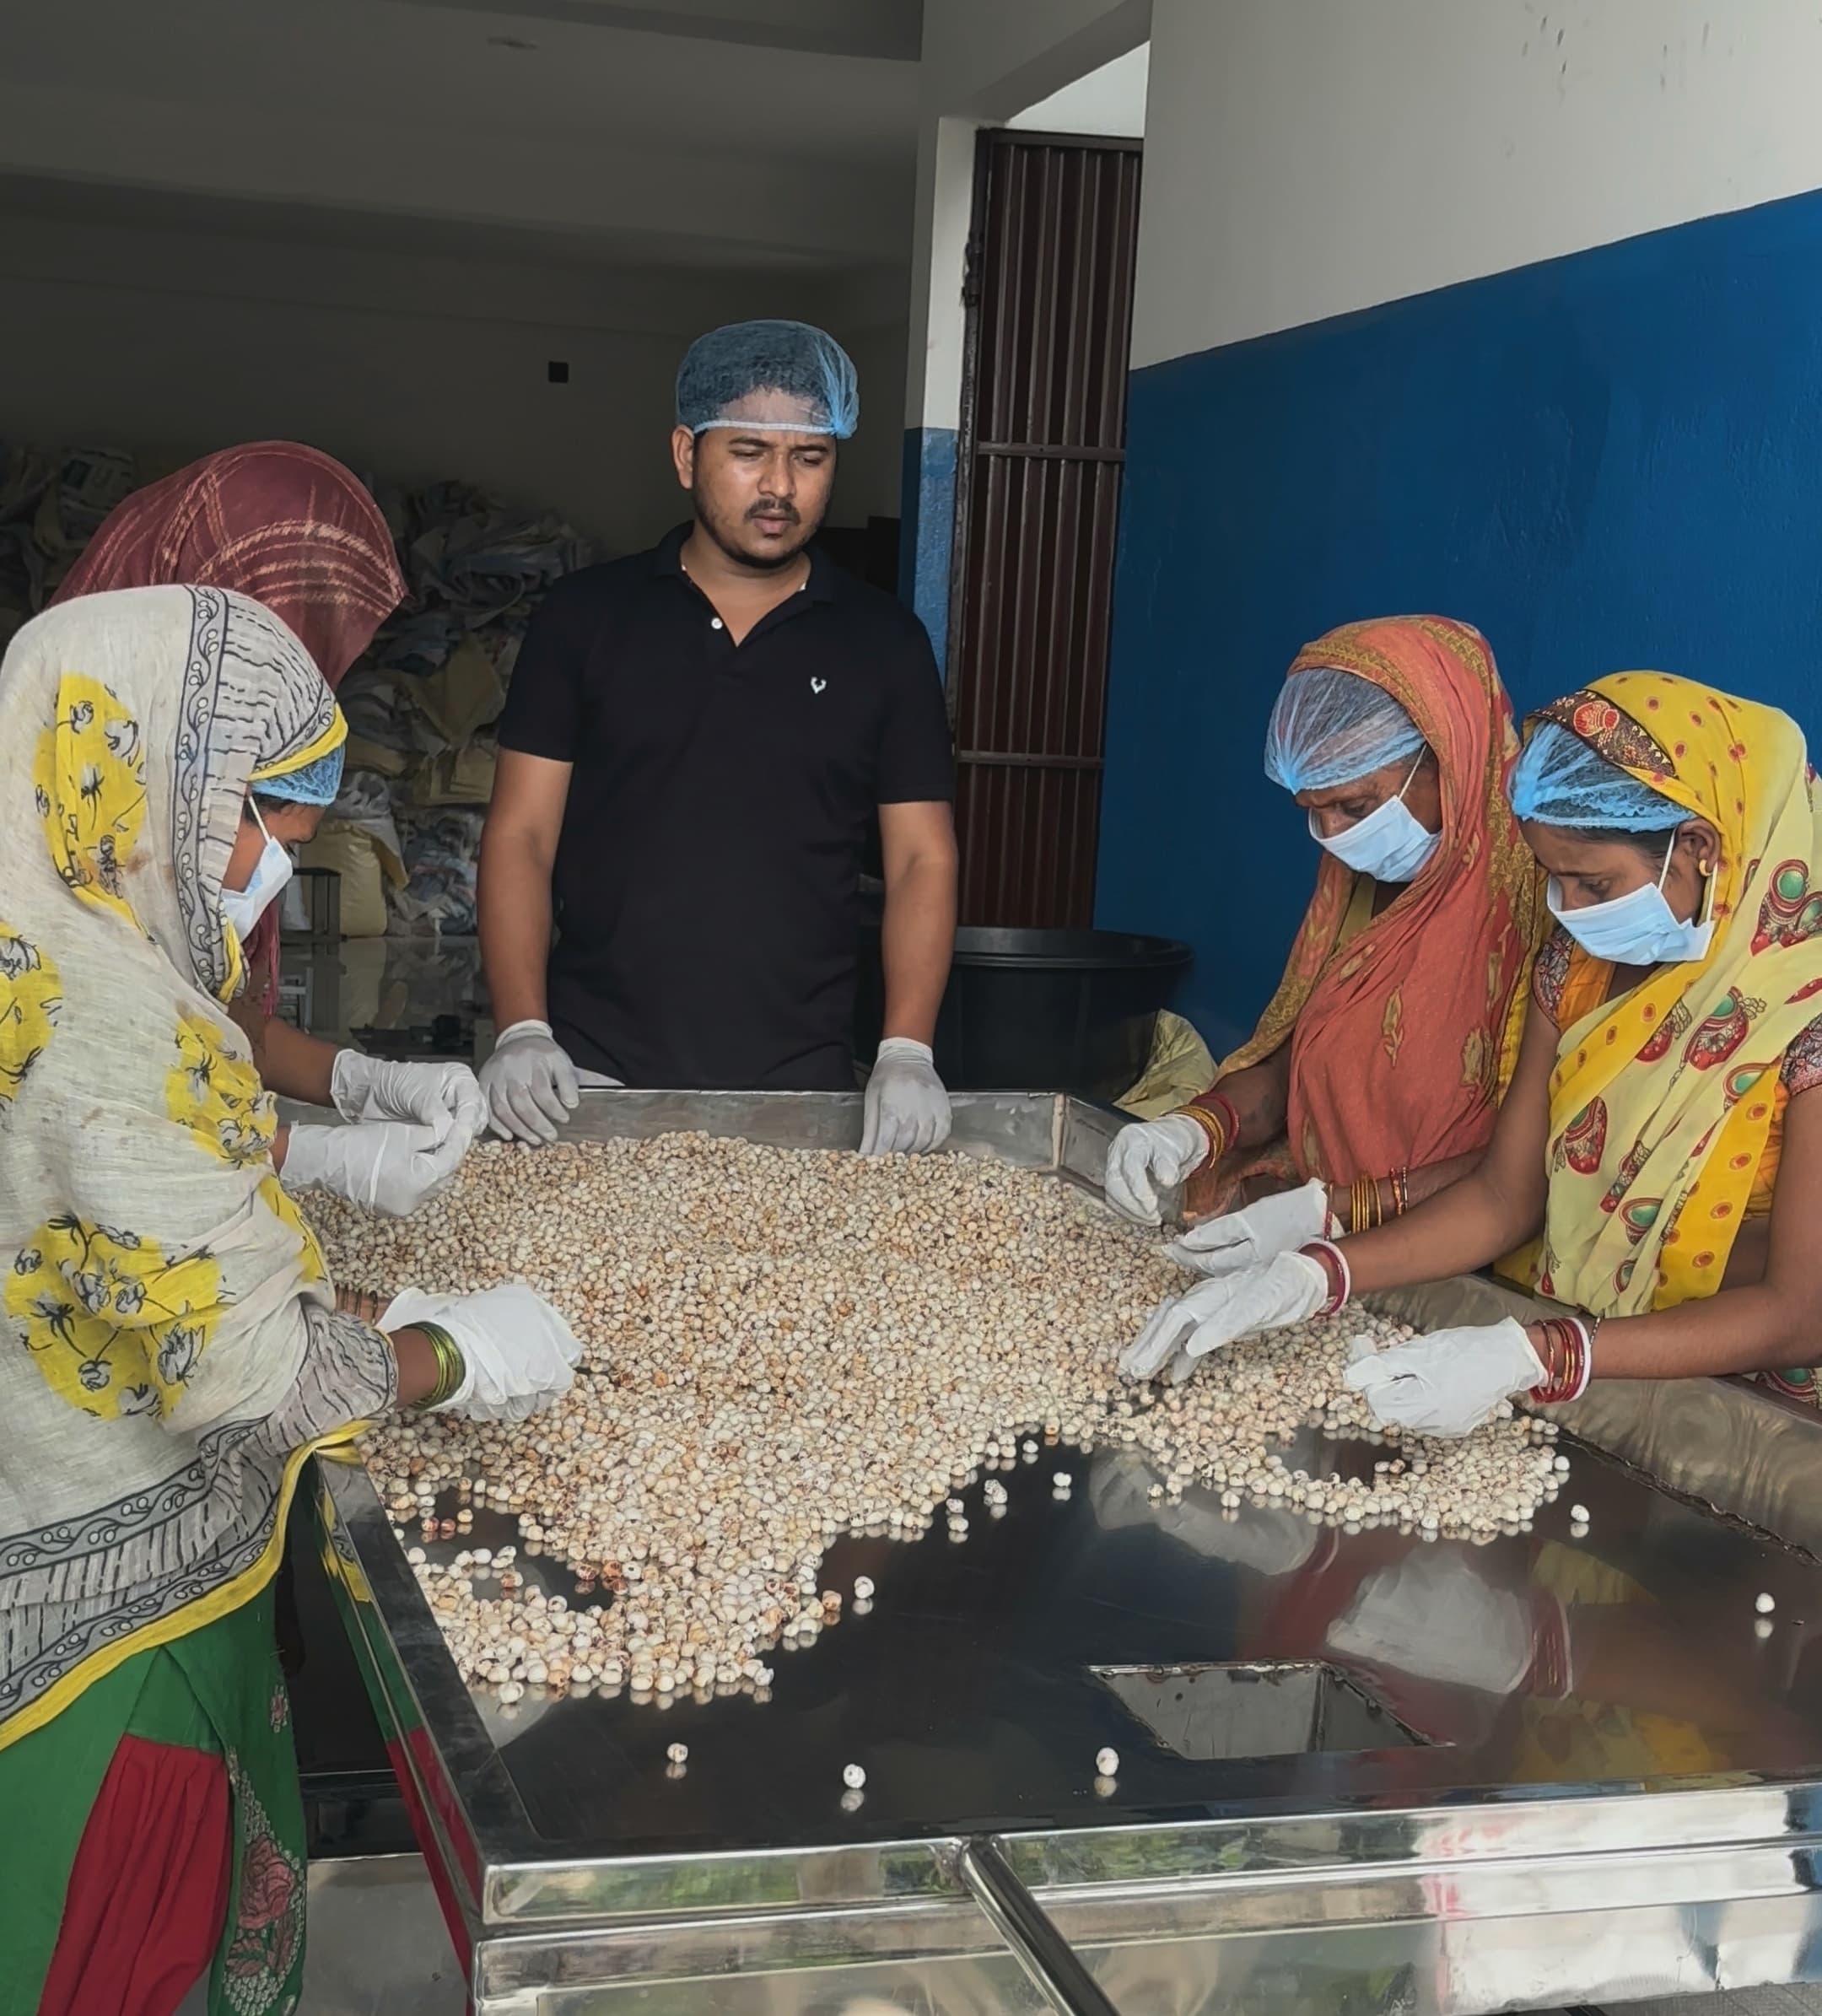
Coating MechanismMicro-Mist Atomization & Drum Baffles
Drum ConstructionSanitary Mirror-Finish SS 304
Dispersion Accuracy±0.5% Seasoning Distribution Tolerance
Carrier MediumFood-Grade Cold-Pressed Oil (<4% Net)
Standardized Factory SOP
In-Line Laboratory Assay & Moisture Control
Stage 04 • Quality AssuranceCritical Control Point (CCP-2)
EquipmentIn-House QA Testing Lab & Moisture Analyzers
04SOP-LAB-04 / ISO 22000 Protocol
Final Moisture < 3.5% (Crisp Guard)

In-Line Laboratory Assay & Moisture Control

Every production lot undergoes mandatory analytical validation in our Katihar plant QA laboratory. Technicians evaluate moisture percentages via halogen moisture analyzers, screen for aflatoxins and peroxide values, conduct organoleptic crunch sensory panels, and verify zero foreign material before releasing the lot for packaging.
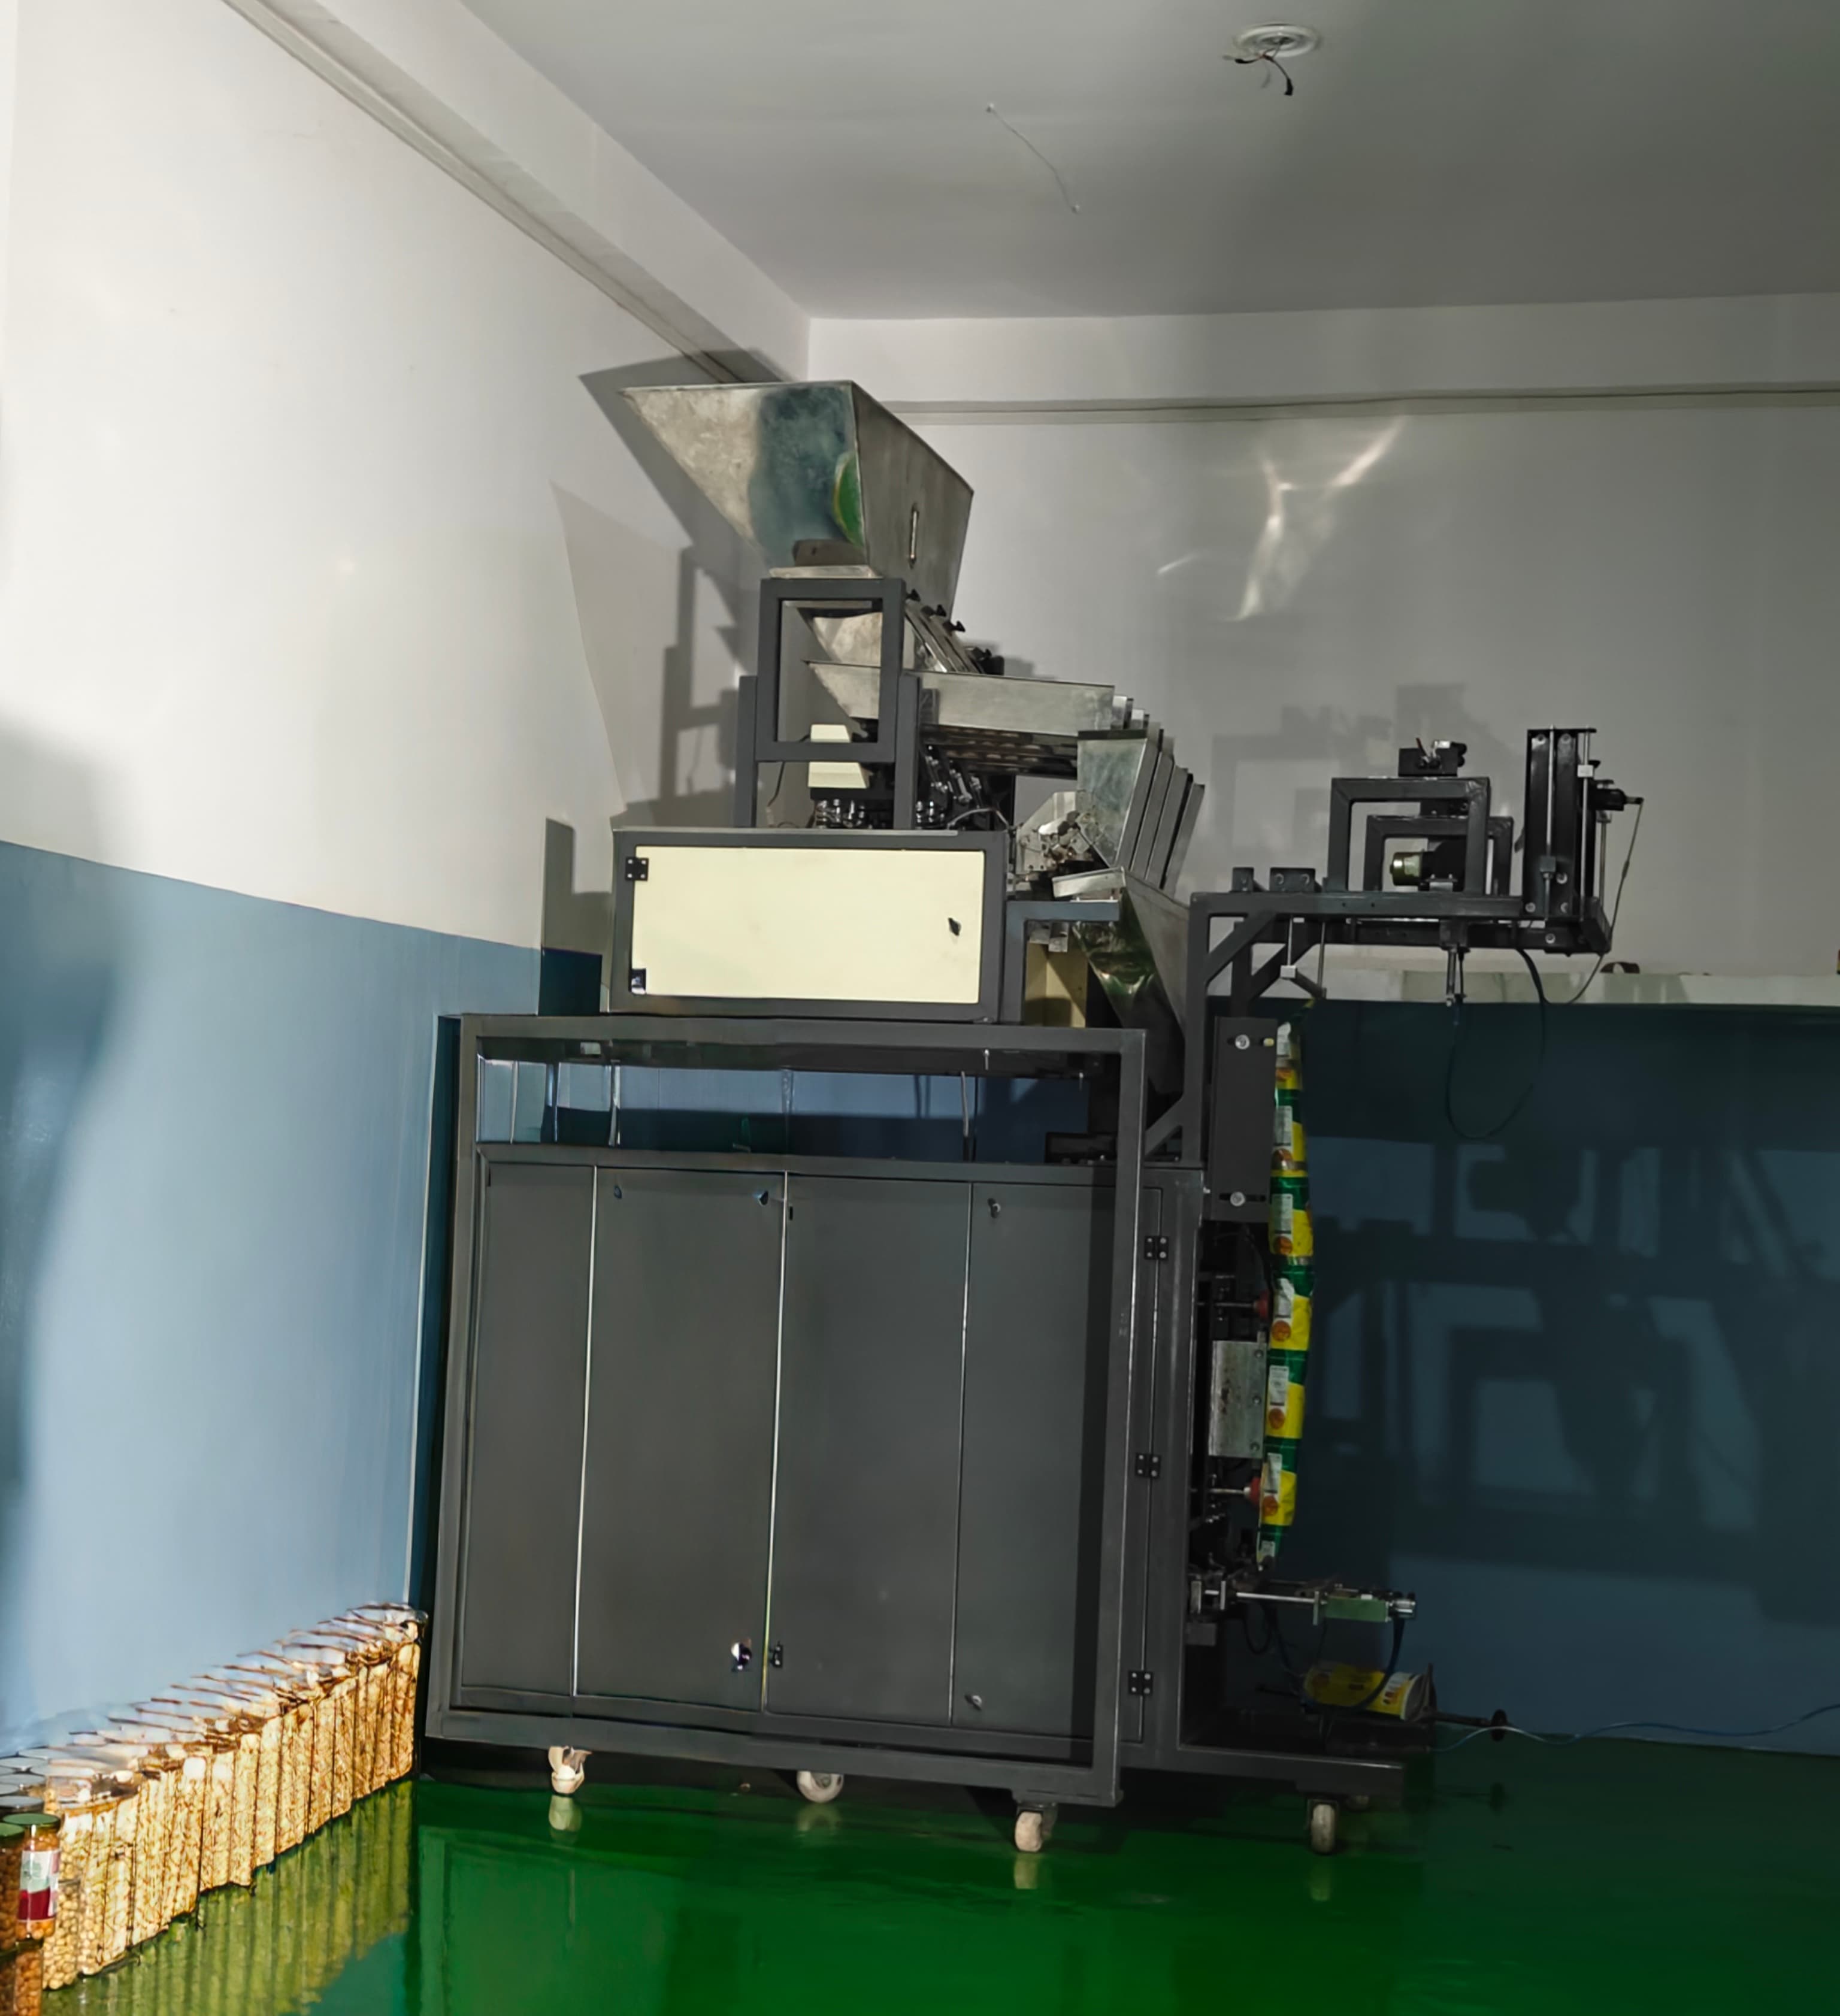
Moisture Standard< 3.5% Critical Threshold
Aflatoxin AssayHPLC Tested (< 4 ppb Total)
Microbiological SpecZero Salmonella, E. Coli, or Coliforms
Traceability ProtocolBarcoded Batch Records (2-Year Archive)
Standardized Factory SOP
High-Speed Automated Multi-Head Packing (VFFS)
Stage 05 • Primary PackagingAutomated Checkweigh Gate
EquipmentComputerized Multi-Head Weigher & VFFS Packaging Unit
05SOP-PKG-05 / Net Content Reg.
±0.2g Net Weight Precision

High-Speed Automated Multi-Head Packing (VFFS)

Our automated packing bays deploy high-precision multi-head combination weighers integrated with vertical form-fill-seal (VFFS) bagging machines. Foxnuts are weighed with milligram precision, dropped through sanitary funnels, and encapsulated into multi-layer barrier laminate pouches without human hand contact.
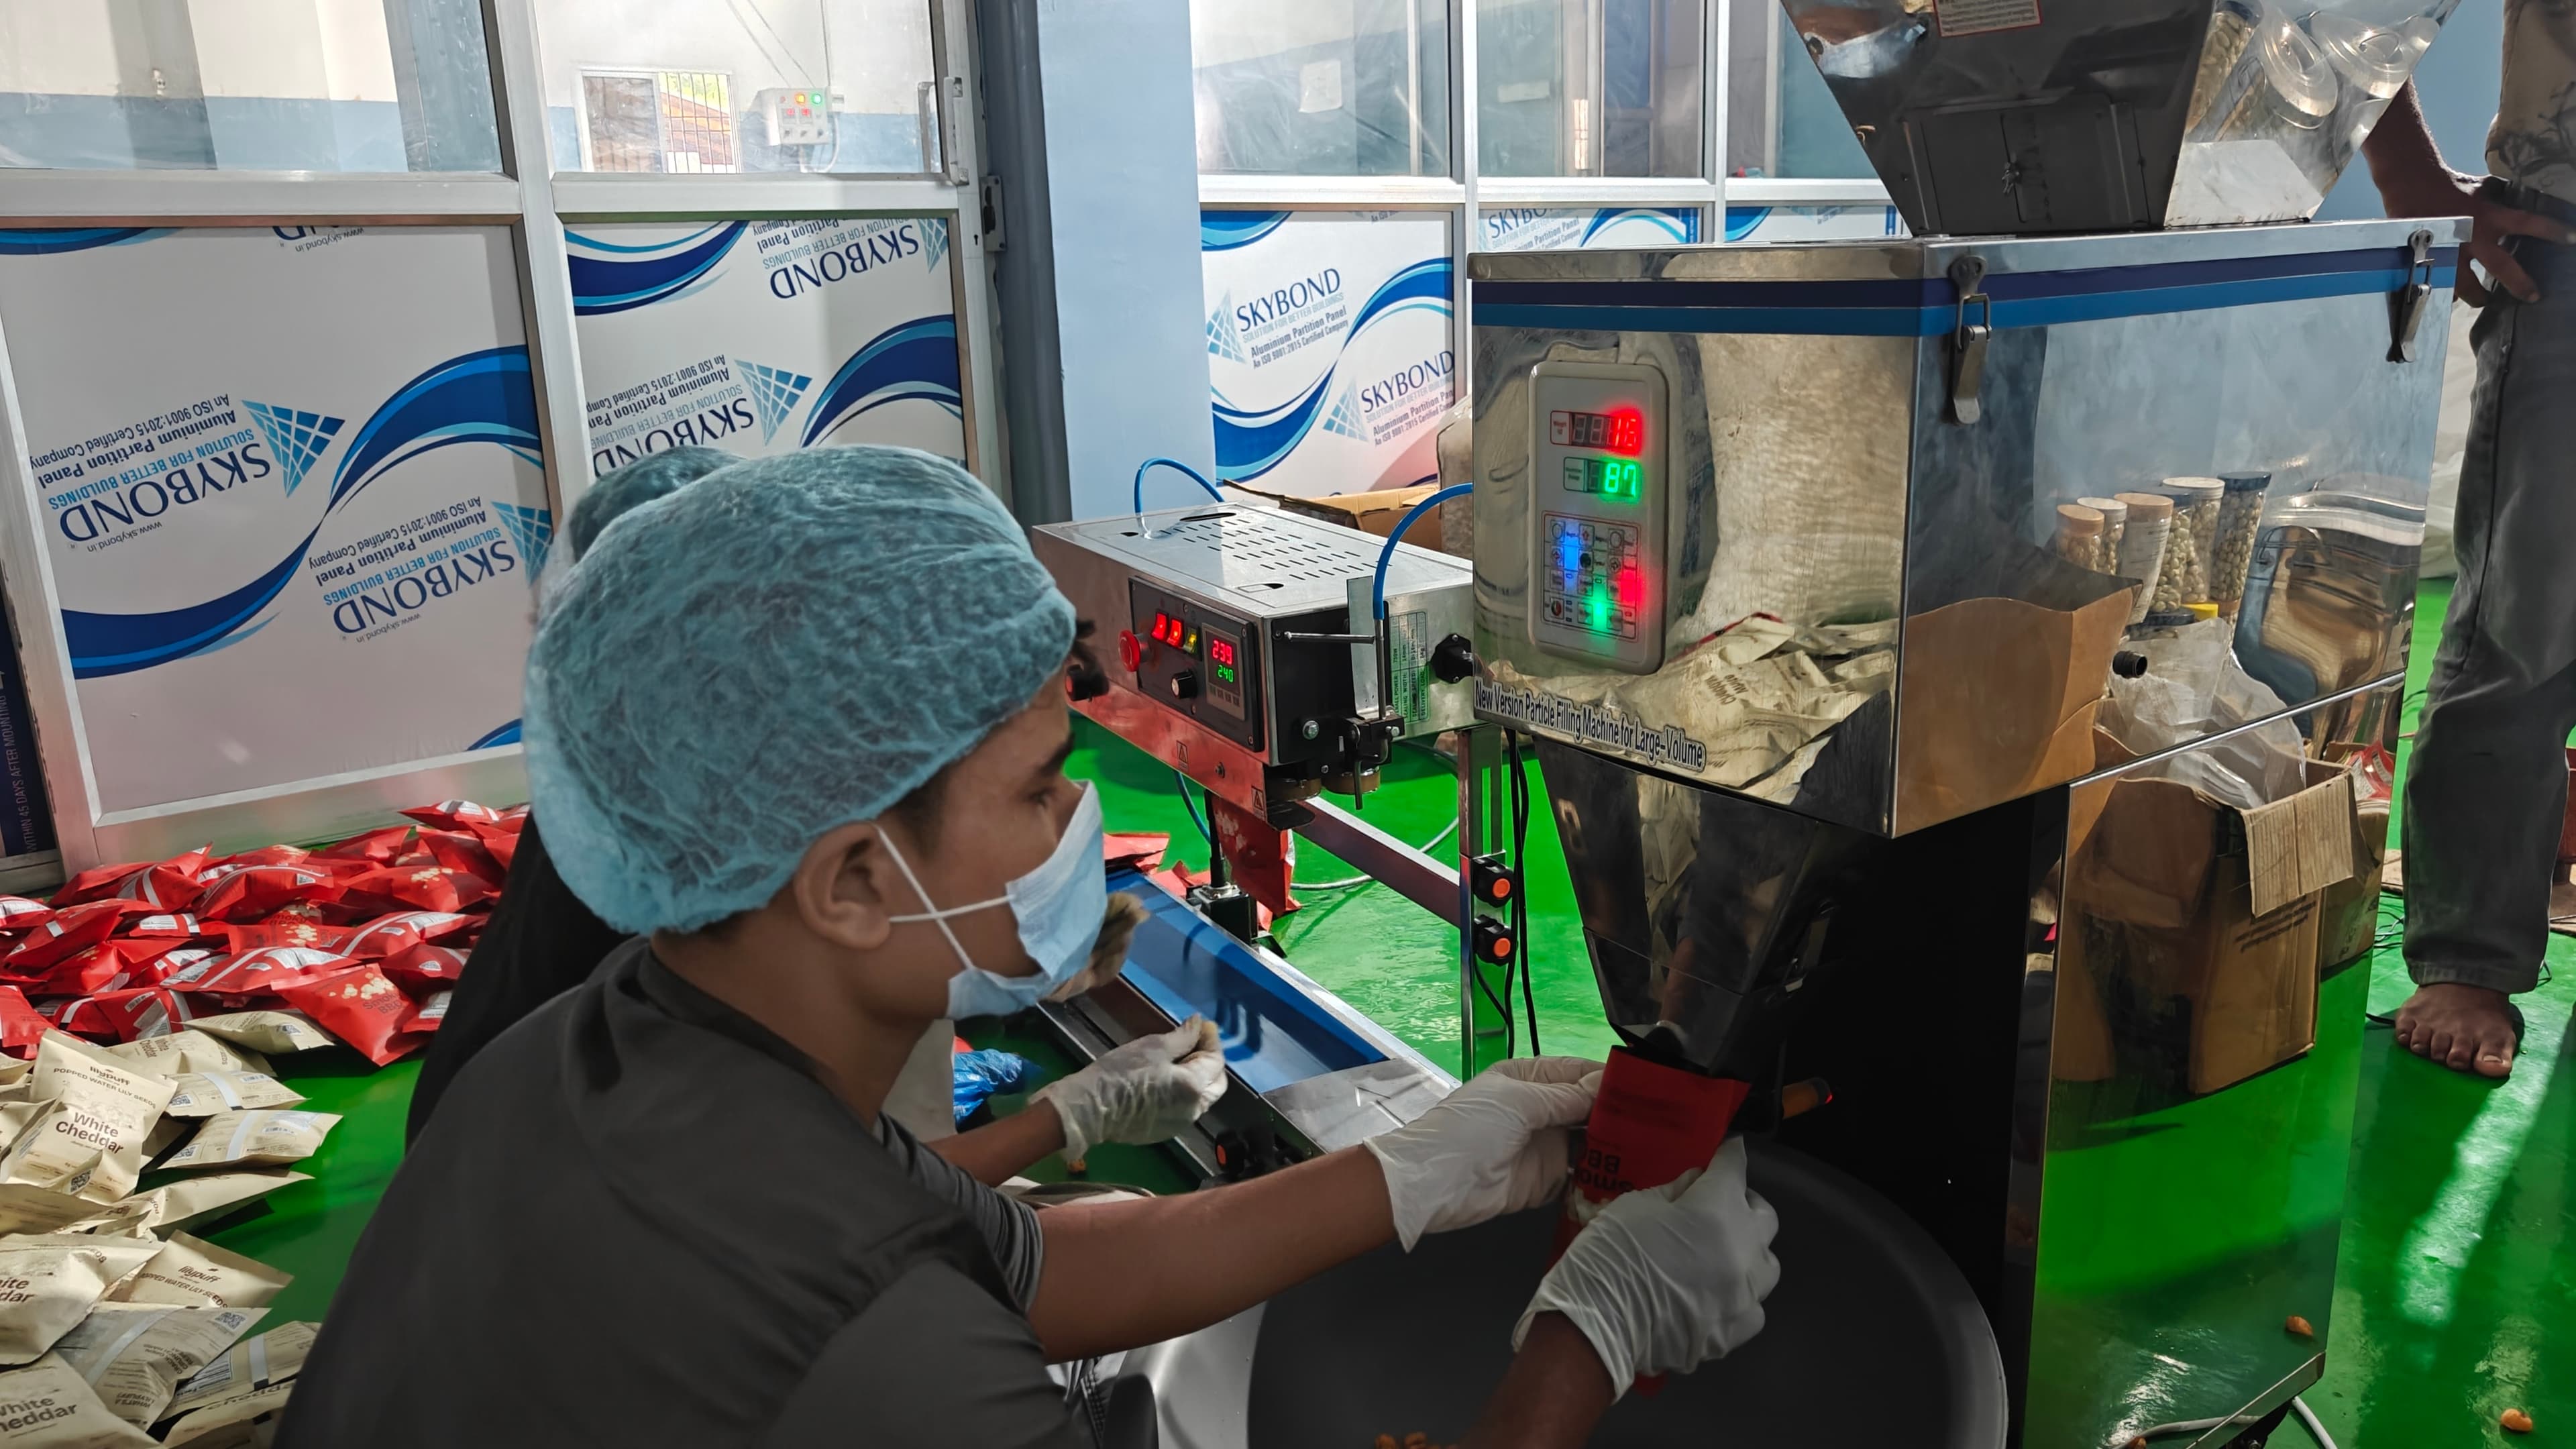
Weigher Type14-Head High-Speed Micro-Computer Weigher
Speed / Output50 to 75 Pouches / Minute per Line
Barrier Laminate3-Layer Metalized PET / Poly Foil
Touchless Operation100% Fully Automated Machine Encapsulation
Standardized Factory SOP
Nitrogen Flush & Hermetic Heat-Band Sealing
Stage 06 • Shelf-Life PreservationCritical Control Point (CCP-3)
EquipmentContinuous Nitrogen Injection & Band Sealing Line
06SOP-PKG-06 / Hermetic Seal Spec
< 1.5% Residual Oxygen Level

Nitrogen Flush & Hermetic Heat-Band Sealing

To safeguard flavor aromatics and prevent lipid oxidation, each pouch is flushed with 99.9% pure food-grade nitrogen gas right before passing through continuous hermetic heat-band sealers. This preserves that freshly roasted crunch and aroma for 9 to 12 months without chemical preservatives or artificial antioxidants.
Nitrogen Purity99.9% Food-Grade Cryogenic / Generator N2
Oxygen Residual< 1.5% Headspace Gas Target
Seal IntegrityPneumatic Bubble Leak Tested
Guaranteed Shelf Life9 to 12 Months Ambient Stability
Standardized Factory SOP
Cleanroom Quality Audit & Secondary Carton Packing
Stage 07 • Secondary PackagingFinal Human Sensory Inspection
EquipmentCleanroom Packaging Conveyor & Shrink Tunnel
07SOP-SEC-07 / Cleanroom Hygiene GMP
100% Visual Seal & Date Code Audit

Cleanroom Quality Audit & Secondary Carton Packing

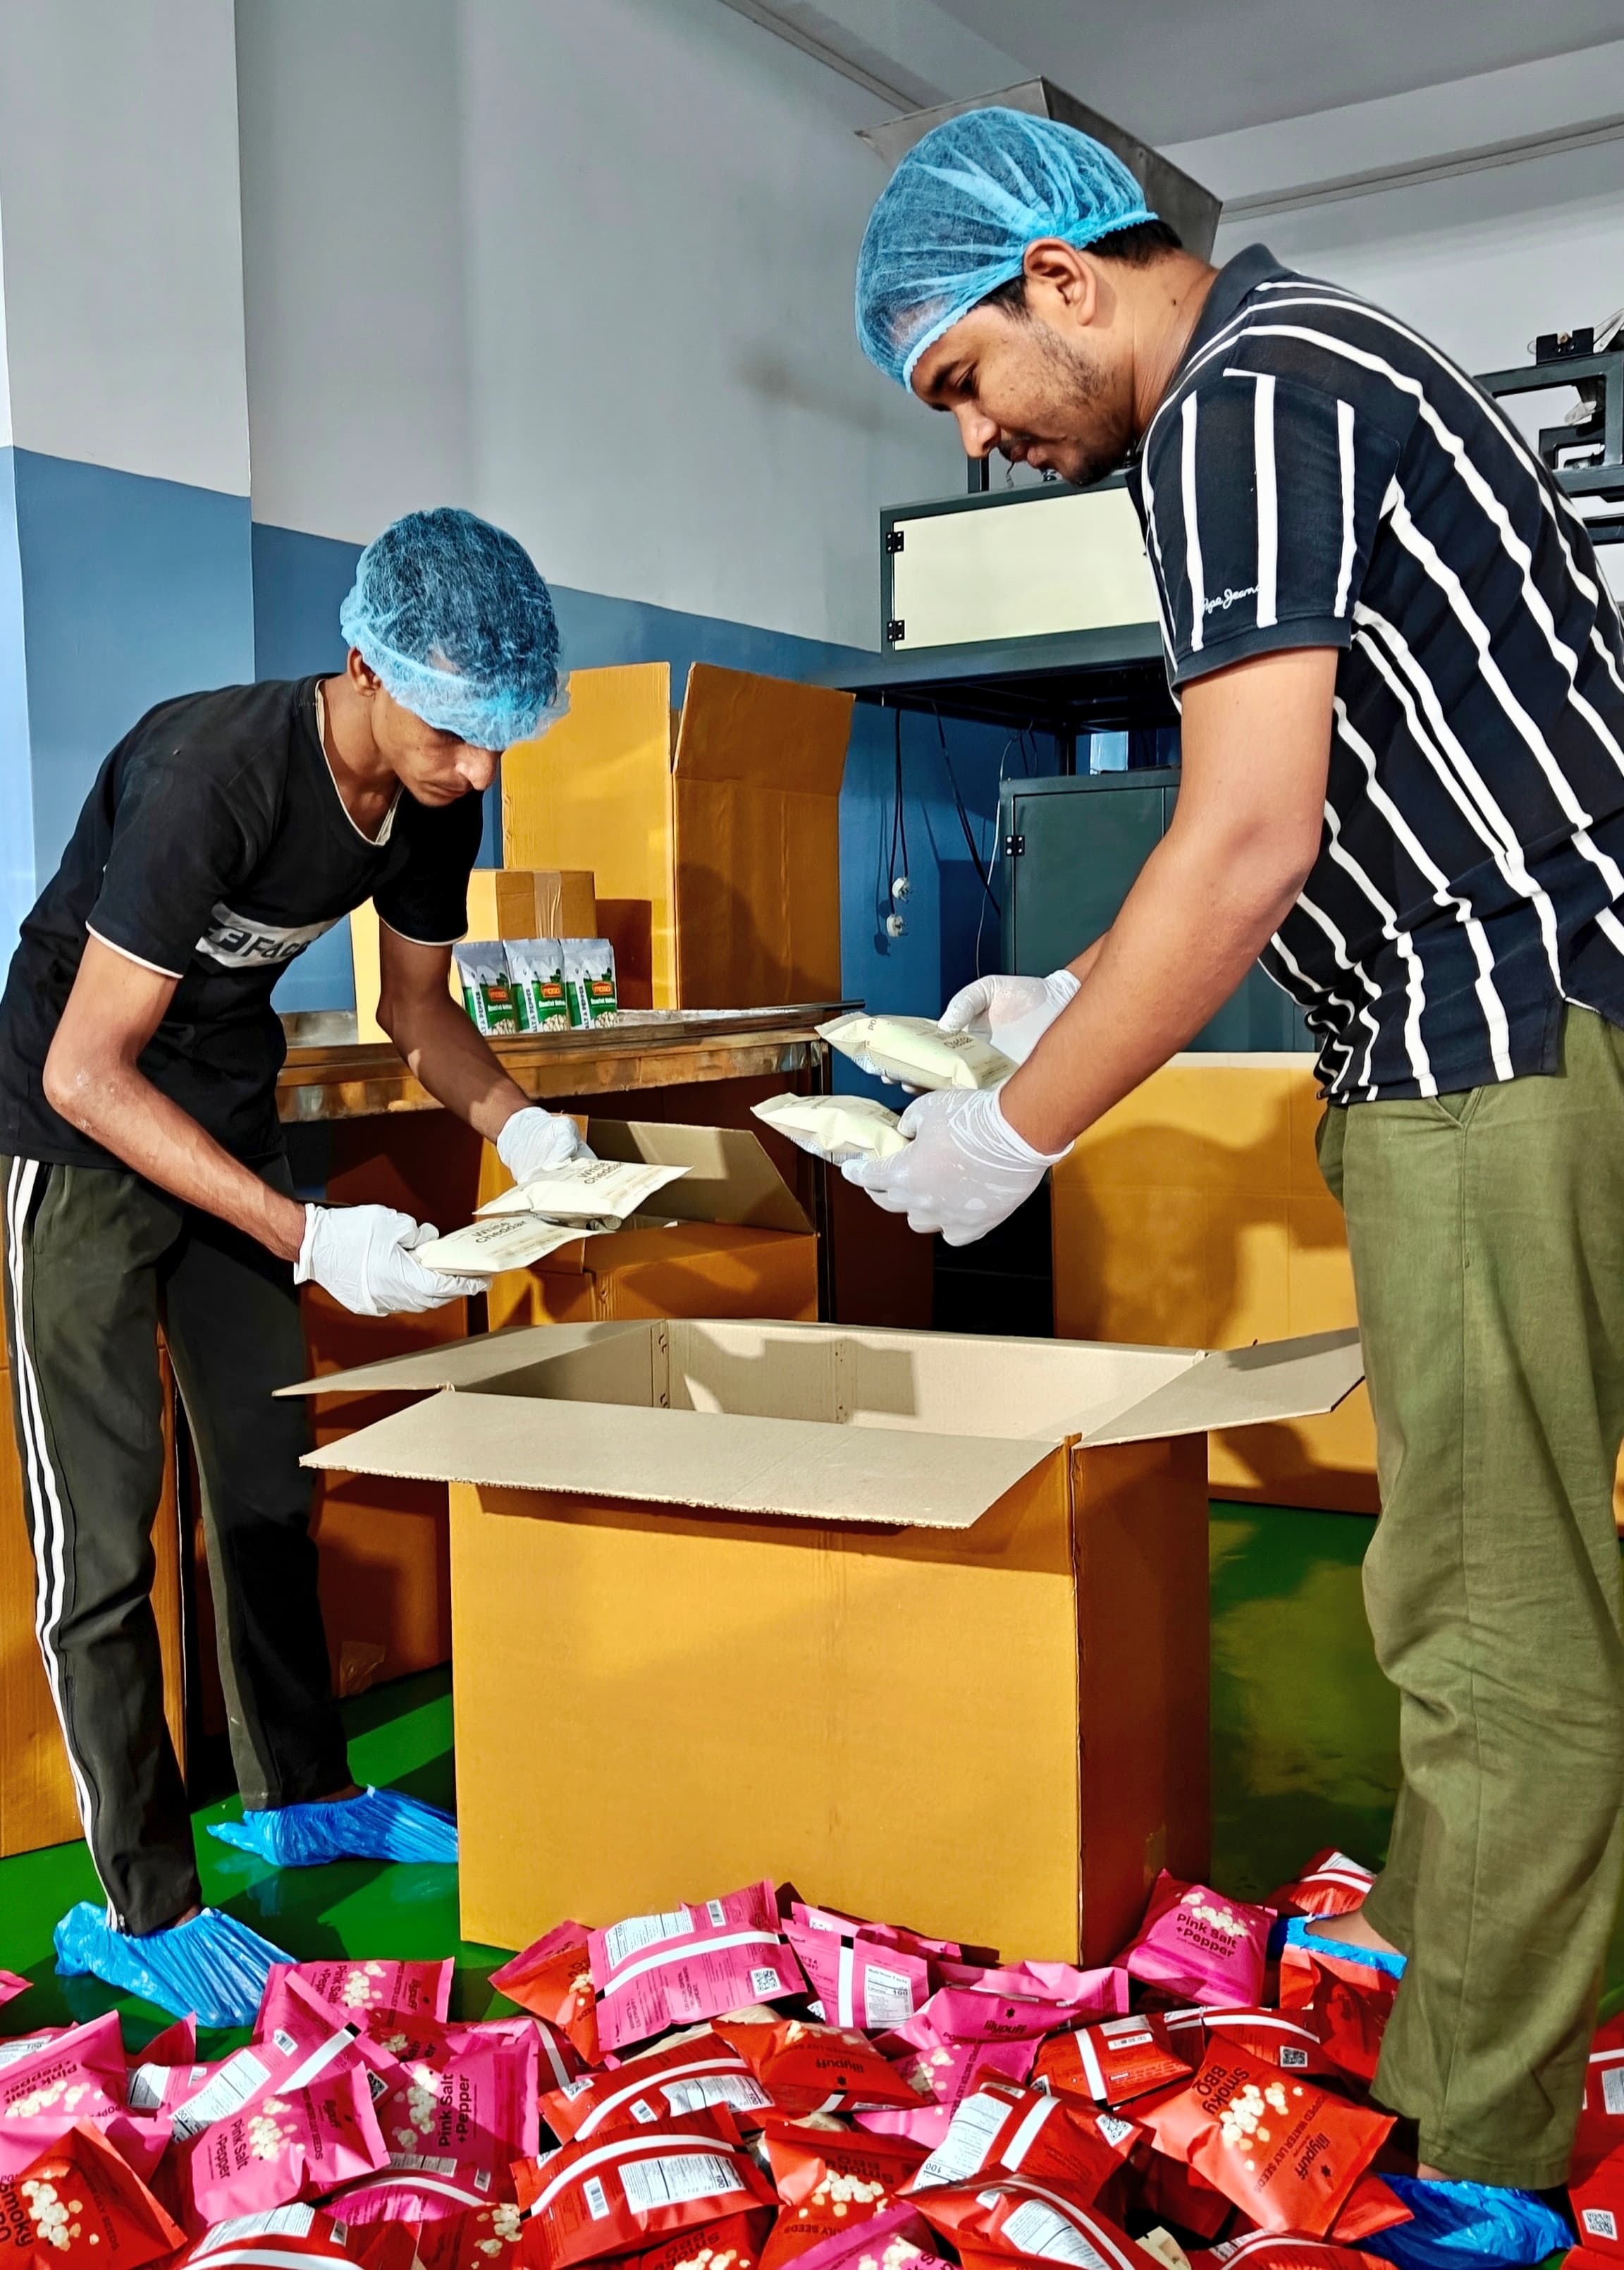
Within our positive-pressure cleanroom zone, trained packaging operators wearing sterile hairnets, aprons, face masks, and medical-grade gloves conduct secondary QA inspection. Every finished pouch is inspected for legible laser batch codes, expiry dates, seal tightness, and packed into master shippers with moisture desiccants.
Hygiene StandardGMP Class 8 Equivalent Cleanroom Zone
Code VerificationBatch, MRP, EXP & QR Code Verification
Carton BundlingHeavy-Duty 5-Ply Corrugated Master Cases
Moisture ProtectionFood-Safe Silica Gel Inclusions per Case
Standardized Factory SOP
Palletized Storage & Warehouse Bay
Stage 08 • Warehousing & StagingWarehouse Storage Audit
EquipmentHeavy-Duty Pallet Racking & Electric Stacker Fleet
08SOP-WHS-08 / Finished Goods Control
Lot-Controlled FIFO Inventory

Palletized Storage & Warehouse Bay

Finished master cartons are stacked on fumigated heat-treated export pallets (ISPM-15 compliant) and stretch-wrapped to prevent ambient moisture ingress. Racks are organized by flavor, batch identifier, and destination market with systematic First-In-First-Out (FIFO) barcoded warehouse management.
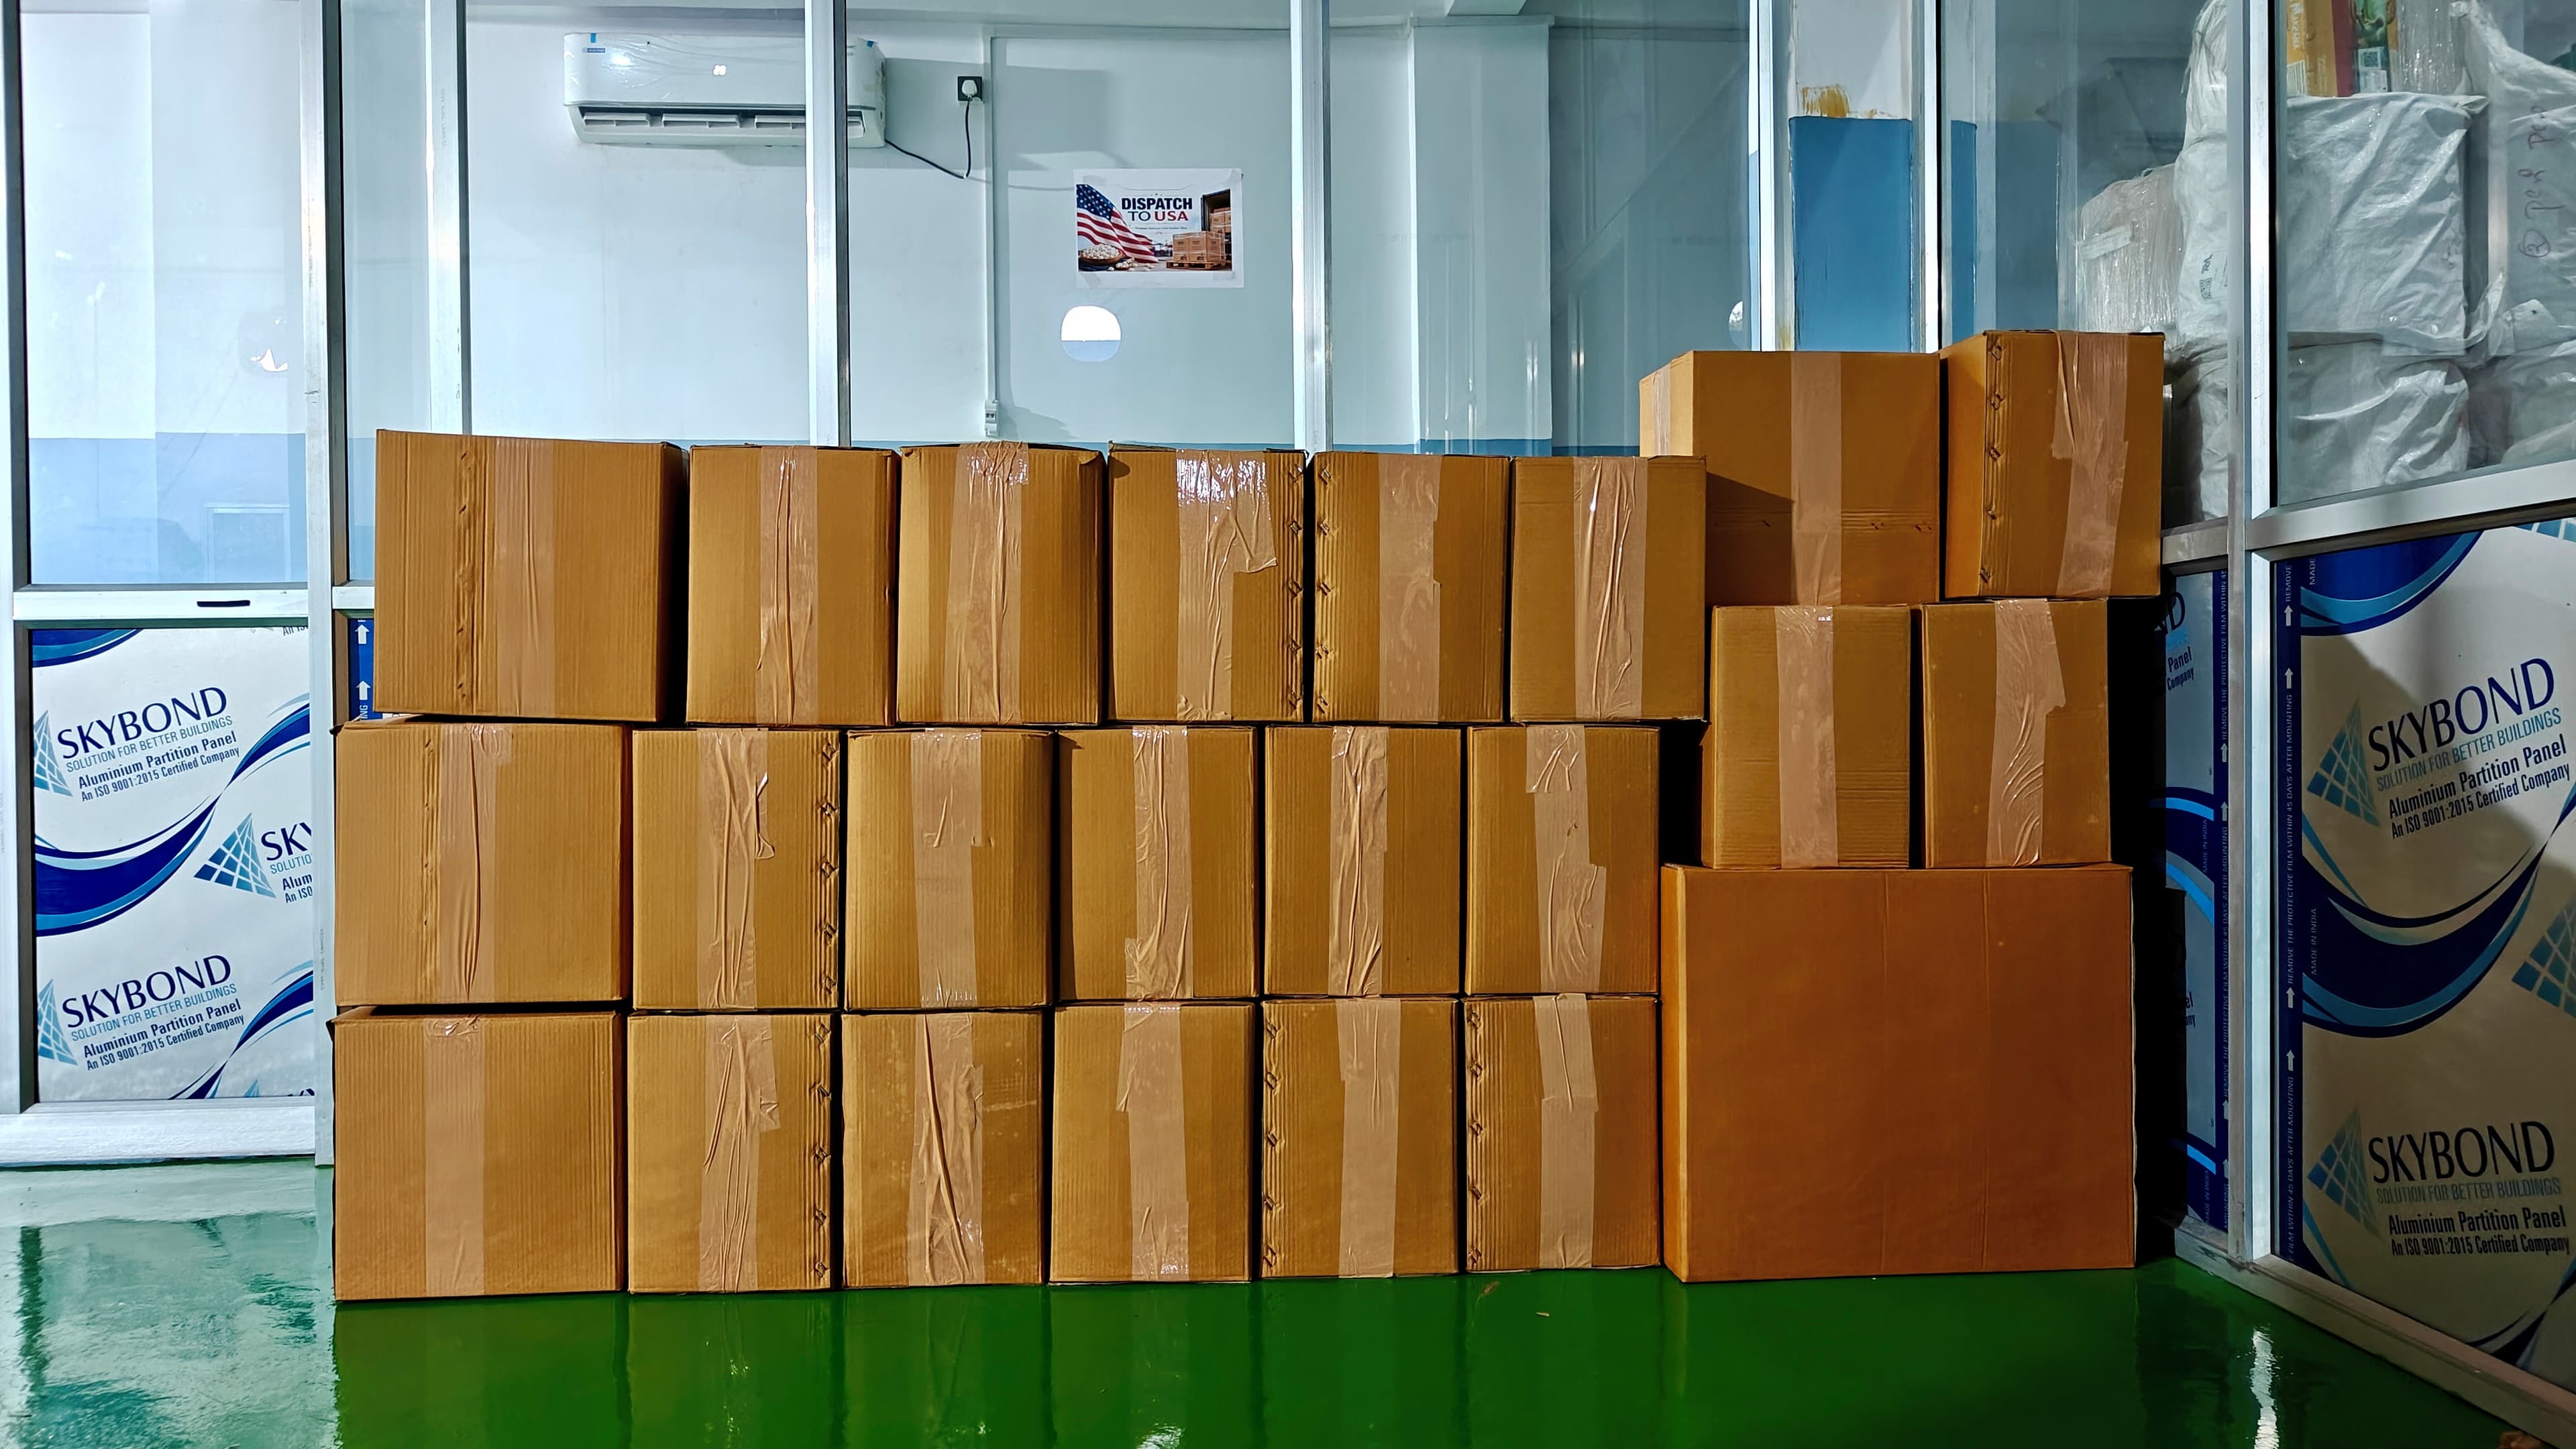
Storage ConditionCool, Dry & Ventilated (<60% RH)
Pallet StandardEuro / ISO Standard Heat-Treated Pallets
Inventory LogicReal-Time WMS Barcode Lot Tracking
Staging Capacity50+ Metric Tons Finished Goods Bay
Standardized Factory SOP
Pan-India Freight & Global Container Logistics
Stage 09 • Dispatch & Outbound LogisticsDispatch Clearance Gate
EquipmentDedicated Outbound Transport Fleet & Container Docks
09SOP-LOG-09 / Container Freight Protocol
Direct Roaster Dispatch from Katihar

Pan-India Freight & Global Container Logistics

Strategically situated in Katihar, Bihar with immediate access to national highways and trans-shipment rail lines, our outbound fleet transports palletized shipments directly to major Indian metropolitan hubs and dry ports (ICDs) / Kolkata/Haldia ports for ocean container freight to North America, Europe, the Middle East, and Asia-Pacific.

Dispatch PointDirect Roaster Facility, Katihar, Bihar
Domestic Transit1–2 Days East India • 3–5 Days Pan-India
Export Handling20ft & 40ft High-Cube Ocean Containers
DocumentationPhytosanitary, Certificate of Origin, Lab COA
Standardized Factory SOP
On-Site Factory Visit Request

Book On-Site Plant Visit

We welcome snack brand founders, institutional procurement officers, wholesale distributors, and export auditors to visit our 12,000+ sq. ft. continuous roasting, automated seasoning, and cleanroom packaging facility in Katihar, Bihar.

Katihar, Bihar Campus Mon - Sat (10:00 AM – 5:00 PM) USFDA & GMP Cleanroom Attire Provided
0 / 50 words max

Please keep description concise (maximum 50 words). Our plant security issues entry passes based on stated purpose.

Entry passes are issued free of cost for verified business buyers.